How to Choose the Right Corrugated Roll?
Choosing the right Corrugated Roll is a production decision, not a simple purchasing task. Roll geometry affects flute formation, bonding, board strength, energy use, and machine stability. A small mismatch can create crushed flutes, uneven pressure, or unstable paper feeding. These defects may appear as weak boxes several hours later.
Industry demand makes this choice increasingly important. Smithers’ “The Future of Corrugated Packaging to 2028” identifies continued growth in corrugated packaging, driven by e-commerce, food delivery, and recyclable transport materials. The Fibre Box Association also reports consistently strong demand for corrugated packaging in North America. More boxes mean greater pressure on corrugator lines, maintenance teams, and quality controls. Every roll must support reliable output, not only impressive speed.
Technical selection should begin with flute profile, roll diameter, paper grade, operating speed, and target board strength. Surface hardness matters. So does groove accuracy. A roll running at high speed may require tighter machining tolerances and better wear resistance. Moisture and temperature also deserve attention, especially when paper properties change between seasons. The correct choice should match actual production conditions, not a supplier’s standard catalogue.
There is no universal Corrugated Roll. A roll suitable for lightweight e-commerce cartons may perform poorly with heavy-duty board. Trial data remains essential. Measure crush resistance, warp, glue quality, vibration, and energy consumption before approving a design. That step can feel slow. It often prevents expensive downtime.
This guide explains the practical factors behind roll selection. It also questions common assumptions, because the fastest option is not always the most economical or reliable.
Define the Corrugated Roll’s Role in Your Production Process
How to Choose the Right Corrugated Roll?
Define the Corrugated Roll’s Role in Your Production Process
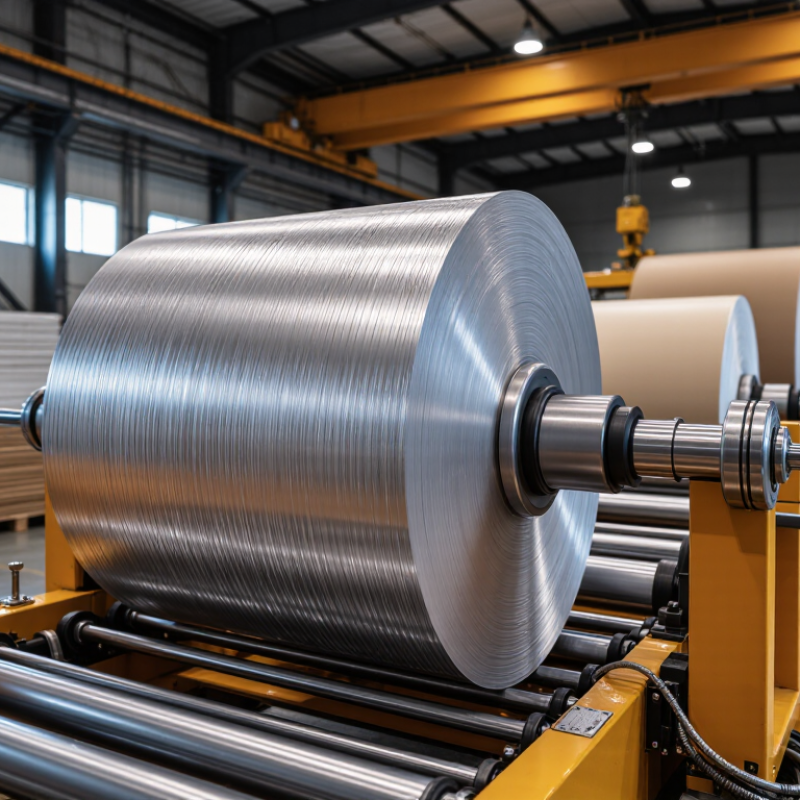
A corrugated roll is not simply a rotating metal part. Its role affects forming accuracy, sheet stability, and production speed. In practice, I begin by identifying its position in the line. Is it shaping the flute, guiding the board, controlling pressure, or supporting material transfer? Each function demands different surface geometry, hardness, and operating limits.
The flute profile must match the board structure and target quality. A roll used for fine flute forming needs precise teeth and stable temperature control. A high-load roll may require stronger materials and better resistance to wear. Check the working width, line speed, paper grade, pressure, and expected operating hours. Small mismatches can create crushed flutes, uneven bonding, or visible board marks. A technically perfect roll can still underperform when the surrounding process is poorly adjusted. I have seen this happen. The roll was blamed first, although pressure settings caused the defect.
Tips: Record roll temperature during production. Inspect flute tips for uneven wear. Compare board samples from the beginning and end of each shift. Ask operators what changes they notice first. Their observations may reveal vibration, noise, or pressure drift before measurements do. Leave room for review. Production conditions often change, and the original roll specification may no longer fit the process.
Match Roll Specifications to Board Grade and Flute Requirements
How to Choose the Right Corrugated Roll?
Match Roll Specifications to Board Grade and Flute Requirements
Selecting a corrugated roll starts with the board grade, not the machine catalog. A lightweight liner needs controlled pressure and accurate flute engagement. Heavier liners may require stronger loading and better heat transfer. Check the medium’s basis weight, moisture level, and fiber stiffness before choosing the roll.
Flute height and pitch also guide the decision. Fine flutes need precise profiles and stable alignment. Larger flutes require deeper teeth and enough space for the medium to form without crushing. Roll diameter affects wrap angle, dwell time, and running speed. Surface finish matters too. A rough surface can mark the liner, while an overly smooth surface may reduce grip.
In production trials, measure flute shape after the board cools. A profile that looks correct at the exit may change later. I have seen good paper fail because the roll gap was adjusted by habit. It was not the paper alone. Check roll wear, bearing condition, steam pressure, and adhesive application together. Small errors can create washboarding, crushed flutes, or weak bonding. Do not rely only on nominal flute dimensions. Actual paper behavior may differ between batches, even under the same grade specification. A trial run with recorded pressure, temperature, speed, and moisture gives a more reliable basis for selection. Perfect calculations still need shop-floor verification.
Evaluate Materials, Surface Design, and Manufacturing Quality
Choosing a corrugated roll starts with the material, not the catalog photograph. Hardened steel suits demanding production and repeated mechanical stress. Tungsten-carbide coatings can resist wear from abrasive papers and mineral fillers. The correct choice still depends on flute profile, speed, steam, and maintenance quality. In my experience, a harder surface cannot rescue poor alignment. Small errors become crushed flutes.
Surface design deserves careful measurement. Check flute geometry, groove consistency, surface roughness, and coating adhesion. A roll may look polished but transfer pressure unevenly across the sheet. Industry statistics from the Fibre Box Association recorded roughly 407 billion square feet of U.S. corrugated shipments in 2023. At that scale, small defects create expensive waste. Smithers’ 2024 market forecast also places global corrugated packaging value above 200 billion dollars by 2028. Demand is growing, but growth does not remove process variation.
Manufacturing quality should be verified with evidence. Request hardness mapping, dynamic-balance results, dimensional records, and runout measurements. ISO 21920 provides a current framework for surface-texture evaluation. ISO 1101 supports geometric tolerancing and clearer inspection requirements. Ask how the manufacturer controls coating thickness at the roll edges. That area is often neglected. I would also test a production sample after several hours, not only during acceptance. Laboratory results can be clean. Your mill may be dusty, humid, and less forgiving.
How to Choose the Right Corrugated Roll
Compare common technical targets before selecting a corrugated roll. Higher surface hardness generally improves wear resistance, controlled roughness supports stable paper traction, and low radial runout helps maintain uniform flute formation and pressure distribution.
Compare Performance, Maintenance Needs, and Operating Costs
How to Choose the Right Corrugated Roll?
A corrugated roll should match your board grade, production speed, and heating system. Performance begins with flute accuracy. A stable flute profile supports consistent bonding and reduces crushing at high speed. Surface finish also matters. A rough or damaged surface can leave uneven marks on the liner.
In plant trials, I compare board strength, line speed, and temperature stability before selecting a roll. Maintenance needs can change the decision. Rolls with durable surfaces usually resist wear, but they still need regular cleaning and alignment checks. Small deposits around the flute tips can affect pressure quickly. I once underestimated this issue, and waste increased before the fault became obvious. That experience changed how I schedule inspections.
Tips: Record roll temperature, vibration, and board moisture each shift. Check flute wear with a calibrated gauge, not visual judgment alone. Compare repair intervals over several months. A cheaper roll may create higher operating costs through energy use, downtime, and rejected sheets. However, premium construction is not always necessary. A medium-duty roll can perform well on stable, moderate-speed lines. The right choice depends on measured conditions, not assumptions.
Review maintenance records with production data. Ask whether cleaning takes minutes or hours. Also consider replacement lead time. A reliable roll is valuable when it keeps the line running during demanding orders.